If you are interested in financing to fund your Bay-Lynx purchase, we recommend that you connect with Easylease Corp., a Canadian-based leasing and finance company that offers premier equipment leasing and financial services. They are focused on making it easier than ever before for companies to overcome cash flow and resource constraints to acquire the assets they need to grow their business.
Leasing through Easylease Corp. can offer several benefits:
Click here for your Canadian instant lease quote >>
For US customers, Click here for your instant lease application >>
Choosing the right Horizontal Shaft Concrete Mixer begins with the material, not the machine brochure. Concrete remains one of the world’s most widely used construction materials. The Global Cement and Concrete Association reports annual concrete production at roughly 14 billion cubic metres. That scale makes mixing quality a practical issue, not a minor specification. A poorly matched mixer can leave dry pockets, uneven moisture, or excessive residue along the trough.
The first questions should concern output, aggregate size, mix design, and available installation space. A horizontal shaft mixer usually provides strong shearing action and controlled movement across the mixing chamber. This suits stiff concrete, fiber-reinforced mixtures, and many precast applications. However, performance depends on paddle geometry, shaft speed, wear protection, and loading sequence. More power is not always better. It may increase energy use without improving consistency.
Industry guidance supports careful verification. ACI 304R discusses concrete batching, mixing, and transporting practices, while ASTM C94 emphasizes consistency and performance in ready-mixed concrete production. The International Energy Agency also identifies cement production as responsible for about 7% of global energy-related CO2 emissions. Efficient mixing therefore deserves attention, although mixer energy is only one part of the total footprint.
Look for measurable evidence. Ask for batch-cycle data, tested capacity, moisture-control procedures, and service records. Inspect the discharge gate and liners closely. Small gaps can become expensive problems. Operator experience matters too. A technically excellent mixer can still fail when cleaning routines, calibration, or loading habits are ignored. No single model fits every site. The best choice balances throughput, mix quality, maintenance access, safety, and long-term operating cost. Some decisions remain uncertain until the actual materials are tested. That is a limitation worth admitting.
Begin with the concrete, not the mixer. The Global Cement and Concrete Association reports that about 14 billion cubic metres of concrete are produced globally each year. This scale hides major differences between projects. A precast plant may require stiff, low-slump mixes, while a foundation crew may need faster discharge and flexible batch sizes. Record target output per hour, batch volume, slump, aggregate size, and mixing time.
Horizontal shaft mixers suit dense mixes because their paddles create strong horizontal circulation. However, capacity alone does not prove performance. ASTM C94/C94M and ACI 304R emphasize consistent proportions, uniform mixing, and controlled delivery. Test the intended recipe with local sand moisture and aggregate grading. Watch the discharge gate closely. Dry pockets or stone buildup can reveal poor mixing before laboratory results do.
Define acceptable variation before requesting quotations. A practical trial should check slump, air content, visual uniformity, and compressive strength. Measure energy use and cleaning time too. These details affect production more than brochure figures. Industry experience suggests that rushed batch cycles often create hidden quality losses. I have seen operators increase speed, then spend longer correcting uneven loads. That is not real productivity. Leave room for mistakes. Moisture changes during a wet week can defeat an otherwise accurate production plan. Recheck the targets after the first trials.
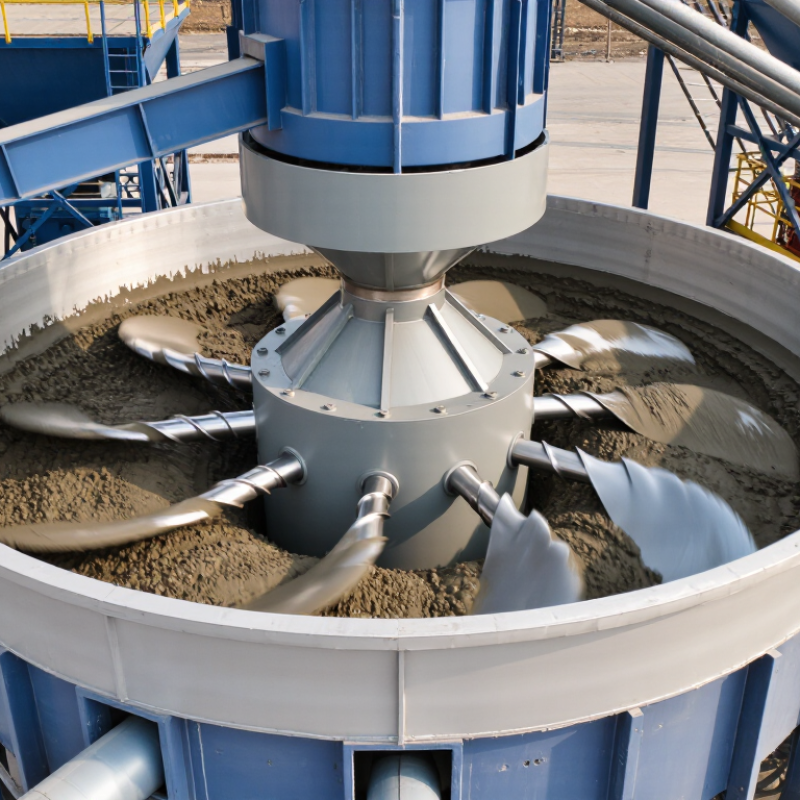
A horizontal shaft concrete mixer uses a fixed trough and rotating shafts to move material through a controlled mixing path. Twin-shaft designs usually create overlapping circulation zones, while single-shaft models rely on paddles or blades to lift and fold the batch. This difference affects mixing speed, moisture distribution, and discharge consistency. A twin-shaft mixer may handle stiff concrete efficiently, but it can demand more power and maintenance. A single-shaft unit is often simpler, yet dead zones may appear if blade clearance is poorly adjusted. Field results can differ.
ACI 304R emphasizes uniform charging, adequate mixing time, and careful moisture control. ASTM C94/C94M also requires concrete to meet specified uniformity and performance requirements. These standards do not select one mixer design. They remind engineers to test the complete process. The Global Cement and Concrete Association reports that cement production contributes about 7% of global carbon dioxide emissions. Efficient mixing, reduced rework, and accurate water dosing therefore matter beyond productivity. The International Energy Agency also identifies process efficiency as a major pathway for reducing cement-sector emissions.
Tips: Compare effective volume, shaft speed, blade geometry, and discharge time. Ask for a trial batch using your actual aggregate grading. Check samples from the front, center, and rear. One test is not enough. Measure power consumption per cubic meter, not only hourly output. A common mistake is choosing by capacity alone. I have seen a large mixer perform poorly when its filling level stayed too low. That detail is easy to miss.
Choosing a horizontal shaft concrete mixer starts with capacity, not appearance. Match batch volume to daily production and feeding methods. A mixer rated for one cubic meter may produce less usable concrete after clearance and material variation. Leave working space for cement, aggregate, water, and safe blade movement. Measure the actual batch, then compare it with the stated capacity. In practice, a modest reserve often prevents overloaded starts. More is not always better.
Power must suit the mix, not simply the motor label. Stiff concrete, large aggregate, and frequent starts demand stronger torque. Check motor output, gearbox design, and overload protection together. A low-power unit may run smoothly empty, then stall under a dense load. That difference matters. Inspect the shaft, paddles, liner, and discharge gate. Wear-resistant steel can extend service life, but material grade alone proves little. Request test data, weld quality, and replacement-part dimensions. I once focused too much on plate thickness and overlooked poor maintenance access.
Mixing performance depends on blade layout, shaft speed, and loading order. Look for uniform texture without dry pockets or water pooling. Run a timed trial with your intended recipe, not a showroom mixture. Take samples from the beginning, middle, and end of discharge. Consistent color and slump suggest better distribution, although laboratory testing remains more reliable. Cleanout time also affects productivity. A mixer that traps hardened concrete can quietly increase labor and downtime. Review these results with an experienced operator before purchasing.
Evaluate nominal batch capacity, installed drive power, typical mixing time, and material suitability.
How to read this chart: Larger batches generally require more drive power and longer mixing times. The values shown are typical engineering reference points for horizontal-shaft mixers handling ordinary concrete with aggregates up to approximately 40 mm. Confirm the final selection against aggregate size, moisture content, slump, loading method, and required uniformity. Abrasive materials benefit from replaceable wear liners and hardened mixing components.
Choosing a horizontal shaft concrete mixer starts with the installation area, not the mixing capacity. Measure the full footprint, including service space around the drive, discharge gate, and inspection covers. Keep at least one clear route for lifting equipment and replacement parts. The floor must be level, strong, and able to resist vibration during heavy batches. Check the electrical supply, water connection, drainage, and ventilation before delivery. I have seen mixers positioned correctly on paper but blocked by a low beam. That mistake delayed installation for several days. Recheck every dimension on site.
Safety features deserve close attention. Look for guarded shafts, emergency stops, interlocked access covers, and clearly marked isolation points. Operators should reach controls without standing beside moving components. A stable platform and non-slip steps also matter when checking the mixer after a batch. Follow the applicable safety standards and the supplier’s installation instructions. Do not rely on appearance alone. A clean guard can still hide a weak hinge or loose fastener. Maintenance access should allow quick cleaning, lubrication, blade inspection, and seal replacement. Leave enough room to remove a shaft bearing without dismantling nearby structures. That detail is often missed. I once accepted a narrow layout, and routine maintenance became unnecessarily slow. A slightly larger service area would have prevented repeated disruption.
| Evaluation Dimension | What to Check | Practical Data or Selection Guidance | Why It Matters | Recommended Decision |
|---|---|---|---|---|
| Required Batch Capacity | Compare the required output with the mixer’s usable working volume rather than its total shell volume. | For consistent mixing, select a usable batch volume that meets the planned batch size without routinely filling the mixer to its maximum rated level. Confirm the manufacturer’s stated capacity for the actual concrete mix. | Overfilling can reduce mixing quality, increase power demand, and accelerate wear on paddles, liners, and drive components. | Choose a model with capacity above the normal batch requirement and allow room for material movement. |
| Foundation and Floor | Inspect the slab condition, flatness, reinforcement, anchor locations, drainage, and allowable bearing capacity. | Use a level, crack-free foundation designed for the mixer’s operating weight, dynamic loads, and vibration. The required bearing capacity and anchor design must be calculated from the selected mixer and local structural requirements. | A weak or uneven base may cause misalignment, excessive vibration, anchor failure, or premature bearing damage. | Obtain a foundation drawing and have the supporting structure verified before ordering. |
| Available Installation Space | Measure the mixer footprint, loading position, discharge position, access routes, and overhead obstructions. | Reserve the equipment footprint plus sufficient working space around inspection covers, lubrication points, electrical panels, and discharge equipment. A clear service aisle of approximately 600–1,000 mm is commonly used where site conditions permit; verify the actual access requirement. | Restricted space makes installation, cleaning, inspection, and emergency response more difficult. | Create a scaled layout showing the mixer, conveyors, platforms, walls, columns, and maintenance routes. |
| Material Feeding Arrangement | Check whether aggregates, cement, water, and admixtures can enter the mixer without blockage or unsafe manual handling. | Confirm inlet height, feed direction, chute or conveyor alignment, dust-control provisions, and the required opening size. Keep the feed path short, stable, and free from unnecessary bends. | Poor feeding arrangements can cause segregation, spillage, dust exposure, and uneven batch loading. | Select inlet dimensions and feed equipment based on the largest aggregate size and the complete batching layout. |
| Discharge Arrangement | Match the discharge gate, outlet height, and discharge direction with the receiving truck, hopper, belt, or pump. | Verify discharge opening dimensions, gate operating space, receiving equipment height, and the required discharge time for the production cycle. | An incompatible outlet can cause concrete buildup, interrupted production, and difficult cleaning. | Confirm the discharge interface using a layout drawing before final equipment selection. |
| Electrical Supply | Check voltage, phase, frequency, motor rating, starting current, control-panel location, and cable routing. | The power supply must match the motor and control equipment nameplate requirements. Provide correctly rated overload protection, short-circuit protection, grounding, and an accessible isolator in accordance with local electrical codes. | Incorrect electrical configuration may cause motor overheating, nuisance trips, unsafe starting, or equipment damage. | Have a qualified electrician confirm the supply and protection scheme before commissioning. |
| Guarding and Interlocks | Inspect guards on the drive, coupling, shaft ends, chains, belts, and other moving parts. | Access covers should be secured and fitted with suitable interlocks or position monitoring where required. The mixer should not operate when a hazardous access door is open. | Rotating shafts and drive components present serious entanglement and crushing hazards. | Reject designs with exposed moving parts or bypassable safety devices. |
| Emergency Stop System | Check the number, location, visibility, and reset method of emergency-stop devices. | Provide clearly identified emergency stops at operator and maintenance access points. After activation, restarting should require a deliberate reset and a separate start command. | Fast access to emergency stopping can reduce the severity of incidents during abnormal operation. | Test every emergency stop during commissioning and include it in routine inspections. |
| Inspection and Cleaning Access | Check access covers, internal lighting, platforms, ladders, washout points, and safe viewing areas. | Inspection openings should allow operators to view wear parts and buildup without reaching into moving equipment. Cleaning access must support isolation, drainage, and safe removal of hardened concrete. | Concrete buildup can reduce capacity, affect mixing performance, and increase mechanical loads. | Prioritize designs that permit cleaning and inspection without entering the mixing chamber. |
| Lockout/Tagout Provision | Confirm that electrical, hydraulic, pneumatic, and stored mechanical energy can be isolated. | Provide a lockable main isolator and documented isolation points. The shaft must be prevented from moving before internal inspection or maintenance begins. | Isolation protects workers from unexpected startup and residual energy. | Require a written lockout/tagout procedure and verify zero energy before servicing. |
| Wear Protection | Review the construction and replaceability of mixing paddles, arms, liners, end plates, and discharge components. | Prefer replaceable wear parts with practical access to fasteners. Wear-resistant liners and paddles should be selected according to aggregate hardness, mix abrasiveness, and operating cycle. | Wear affects mixing uniformity, power consumption, leakage, and service life. | Request wear-part material specifications, replacement procedures, and expected inspection intervals. |
| Lubrication and Bearings | Check bearing locations, grease points, seals, lubrication frequency, and access without removing guards. | Lubrication points should be clearly marked and reachable from a safe position. Use the lubricant type and quantity specified for the installed bearing and operating conditions. | Insufficient or incorrect lubrication is a common cause of bearing overheating and failure. | Select a layout that allows routine lubrication without climbing on the mixer or entering hazardous areas. |
| Noise, Dust, and Water Control | Assess noise sources, cement dust, wash water, drainage, and nearby worker exposure. | Provide suitable enclosure, dust extraction or suppression, splash control, drainage, and housekeeping space. Noise-control measures should be based on a site assessment and applicable occupational limits. | Good environmental control improves worker protection, equipment cleanliness, and regulatory compliance. | Include dust and wash-water management in the installation design rather than adding it after commissioning. |
| Operating Environment | Evaluate ambient temperature, humidity, rain, freezing conditions, corrosive substances, and outdoor exposure. | Specify suitable enclosure and electrical protection for the installation environment. Outdoor equipment may require weather protection, drainage, corrosion protection, and freeze precautions. | Environmental conditions can affect insulation, controls, bearings, seals, and structural components. | State the actual site conditions in the equipment specification and confirm all environmental limits. |
| Maintenance and Spare Parts | Review access to wear parts, bearings, seals, gearboxes, motors, sensors, and control components. | Confirm maintenance clearances, lifting points, removable panels, standard fasteners, recommended spare parts, and documented maintenance intervals. | Easy access reduces downtime and lowers the risk of unsafe improvised repairs. | Choose a mixer with a documented preventive-maintenance schedule and practical replacement procedures. |
| Commissioning and Acceptance | Define checks for rotation direction, empty running, loaded operation, discharge, vibration, temperature, interlocks, and emergency stops. | Commissioning should verify installation alignment, electrical protection, safety functions, lubrication, mixing performance, and abnormal noise or vibration under operating conditions. | Early testing identifies installation errors before they become production or safety problems. | Use a written acceptance checklist and retain test records for future maintenance reference. |
Choosing a horizontal shaft concrete mixer requires more than comparing purchase prices. A low-cost machine may consume more power, require frequent blade replacement, or produce uneven batches. The International Energy Agency estimates that electric motor systems use roughly half of global electricity. Therefore, motor efficiency deserves careful attention. Ask suppliers for motor ratings, typical energy use per batch, mixing-cycle time, and spare-part prices. A ten-minute cycle can become expensive when repeated hundreds of times each week.
Operating efficiency also depends on the material and site conditions. Test the mixer with your actual aggregate size, moisture level, and target slump. Observe the discharge gate closely. Does concrete leave smoothly, or does material remain around the shaft? Small residues become costly when cleaning takes twenty extra minutes after every load. Production records should track batch time, rejected material, electricity use, and maintenance hours. The data may challenge your initial preference. Bigger is not always better.
Supplier support is part of the equipment cost. The U.S. Department of Energy recommends evaluating motor-driven systems through lifetime operating costs, not purchase price alone. Request service response times, maintenance manuals, wear-part availability, and operator training. Check whether technicians can diagnose gearbox, bearing, and hydraulic faults remotely. A supplier can sound convincing during negotiations. Evidence matters more. Still, no quotation reveals every future problem; allowance for downtime remains imperfect, but ignoring it is worse.